Sponsored by RETSCH GmbHReviewed by Olivia FrostOct 1 2026
Refuse-derived fuels (RDF) and other alternative fuels such as plastic residues, biomass, used tires, and processed waste fractions are seeing increasingly widespread use in cement rotary kilns, replacing fossil fuels.
RDFs help reduce greenhouse gas emissions by substituting coal, oil, coal, or natural gas, enabling energy recovery and, in some instances, the recovery of valuable mineral constituents from waste streams.
These secondary fuels must meet clearly defined quality specifications to ensure consistent clinker quality and stable kiln operation. Standardized sample preparation, reliable laboratory testing, and reproducible analytical workflows are, therefore, essential.
Representative Sampling and Homogenizing Alternative Fuels
Refuse-derived fuels and other alternative fuels tend to be heterogeneous, bulky, and difficult to handle. Laboratory subsamples must be demonstrably representative of the original batch to ensure meaningful analytical results. Best practice includes:
- Acquiring increments from various points in the bulk material
- Processing a sufficiently large initial sample mass
- Thorough mixing and splitting, for instance, utilizing the PT 200 or another rotary divider to minimize segregation effects
- Duplicate or triplicate analyses of critical parameters will significantly improve confidence in the results and support an in-depth assessment of material variability.
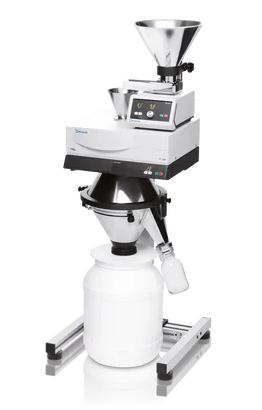
Image Credit: RETSCH GmbH
A Staged Sample Preparation Workflow for RDFs
A typical preparation workflow for RDFs starts with coarse size reduction in a cutting mill (for example, the SM 300) to produce a flowable fraction.
The analytical subsample is milled to the required fineness after remixing and splitting. This is done using a rotor mill such as the Ultra Centrifugal Mill ZM 300. Alternatively, a cross-beater mill (for example, the SK 300) may be used when impact grinding is deemed advantageous.
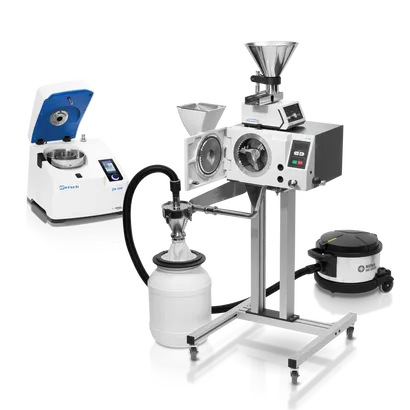
Image Credit: RETSCH GmbH
Target Fineness and Analytical Requirements for RDFs
RDFs’ target fineness should be aligned with the analytical method. For example:
- Calorific value determination typically requires only moderate fineness
- Ash, LOI, and elemental analyses benefit from careful splitting and consistent particle size
- XRF analysis on pressed pellets generally requires finer grinding to improve comparability and minimize particle-size effects
Alternative fuels also introduce mineral components into the kiln system, meaning analytical results are directly relevant to process stability. For example, sulfur and alkalis impact clinker chemistry and emissions control, while chlorine can promote buildups and internal cycles.
Standardized, documented preparation parameters are essential for reproducible data, for example, mill and sieve selection, rotor speed, splitting schemes, and cyclone operation.
Routinely running duplicates and retaining reference subsamples supports reliable RDF qualification and long-term quality control.
Material-Specific Preparation Considerations
Plastic Residues and Tire-Derived Fuels
Film-like, plastic-rich, or tire-derived RDFs require careful temperature control during grinding. Dry-ice embrittlement can prevent smearing and enable efficient size reduction, while cyclone operation supports cooling and rapid discharge.
Leveraging cutting mills for pre-crushing coupled with the Ultra Centrifugal Mill ZM 300 for final grinding is a proven approach to homogenizing these materials.
The use of the six-disk rotor in the pre-cutting step may be more effective than the standard parallel-section rotor, depending on the sample properties (for example, larger or more compact plastic blocks).
Secondary Fuels
40 mm, 50 g
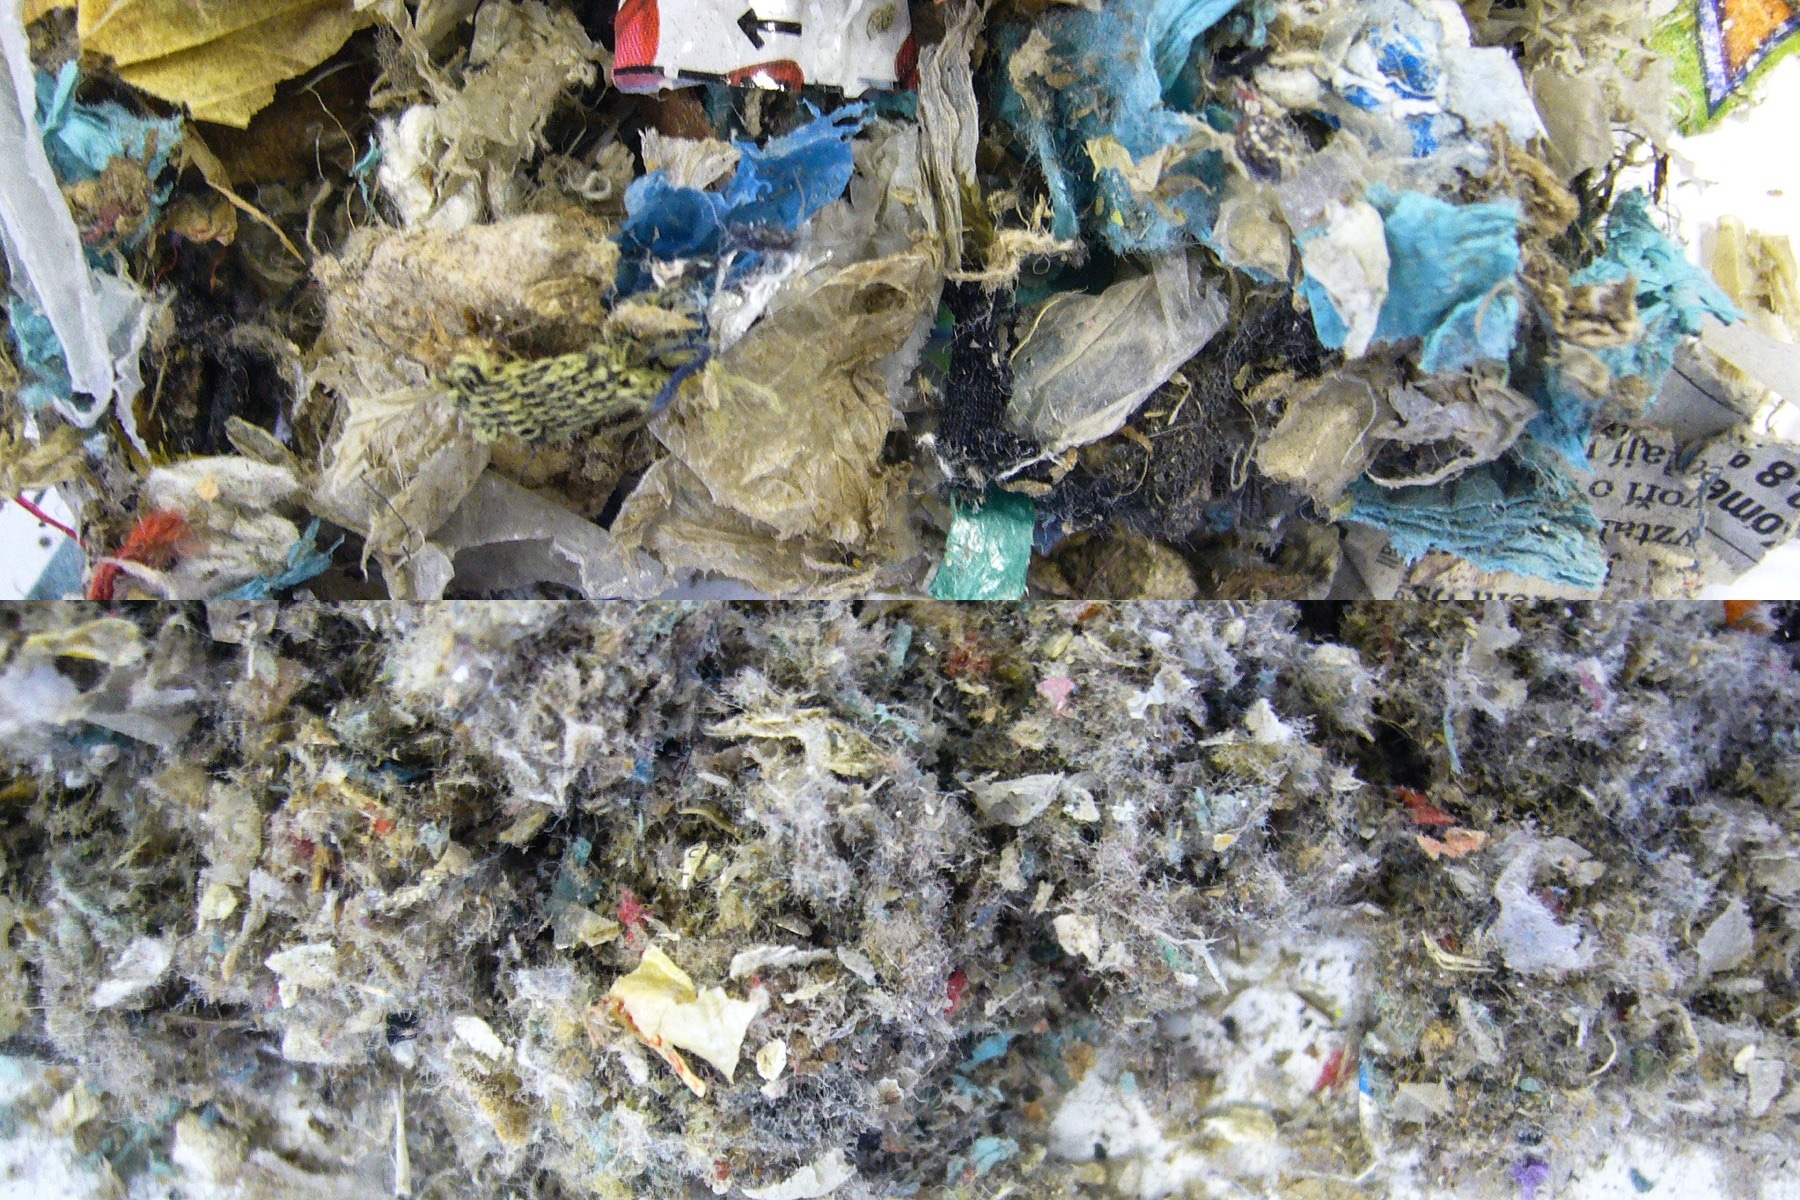
SM 50. Three minutes | 2 mm. Image Credit: RETSCH GmbH
100 mm, 600 g
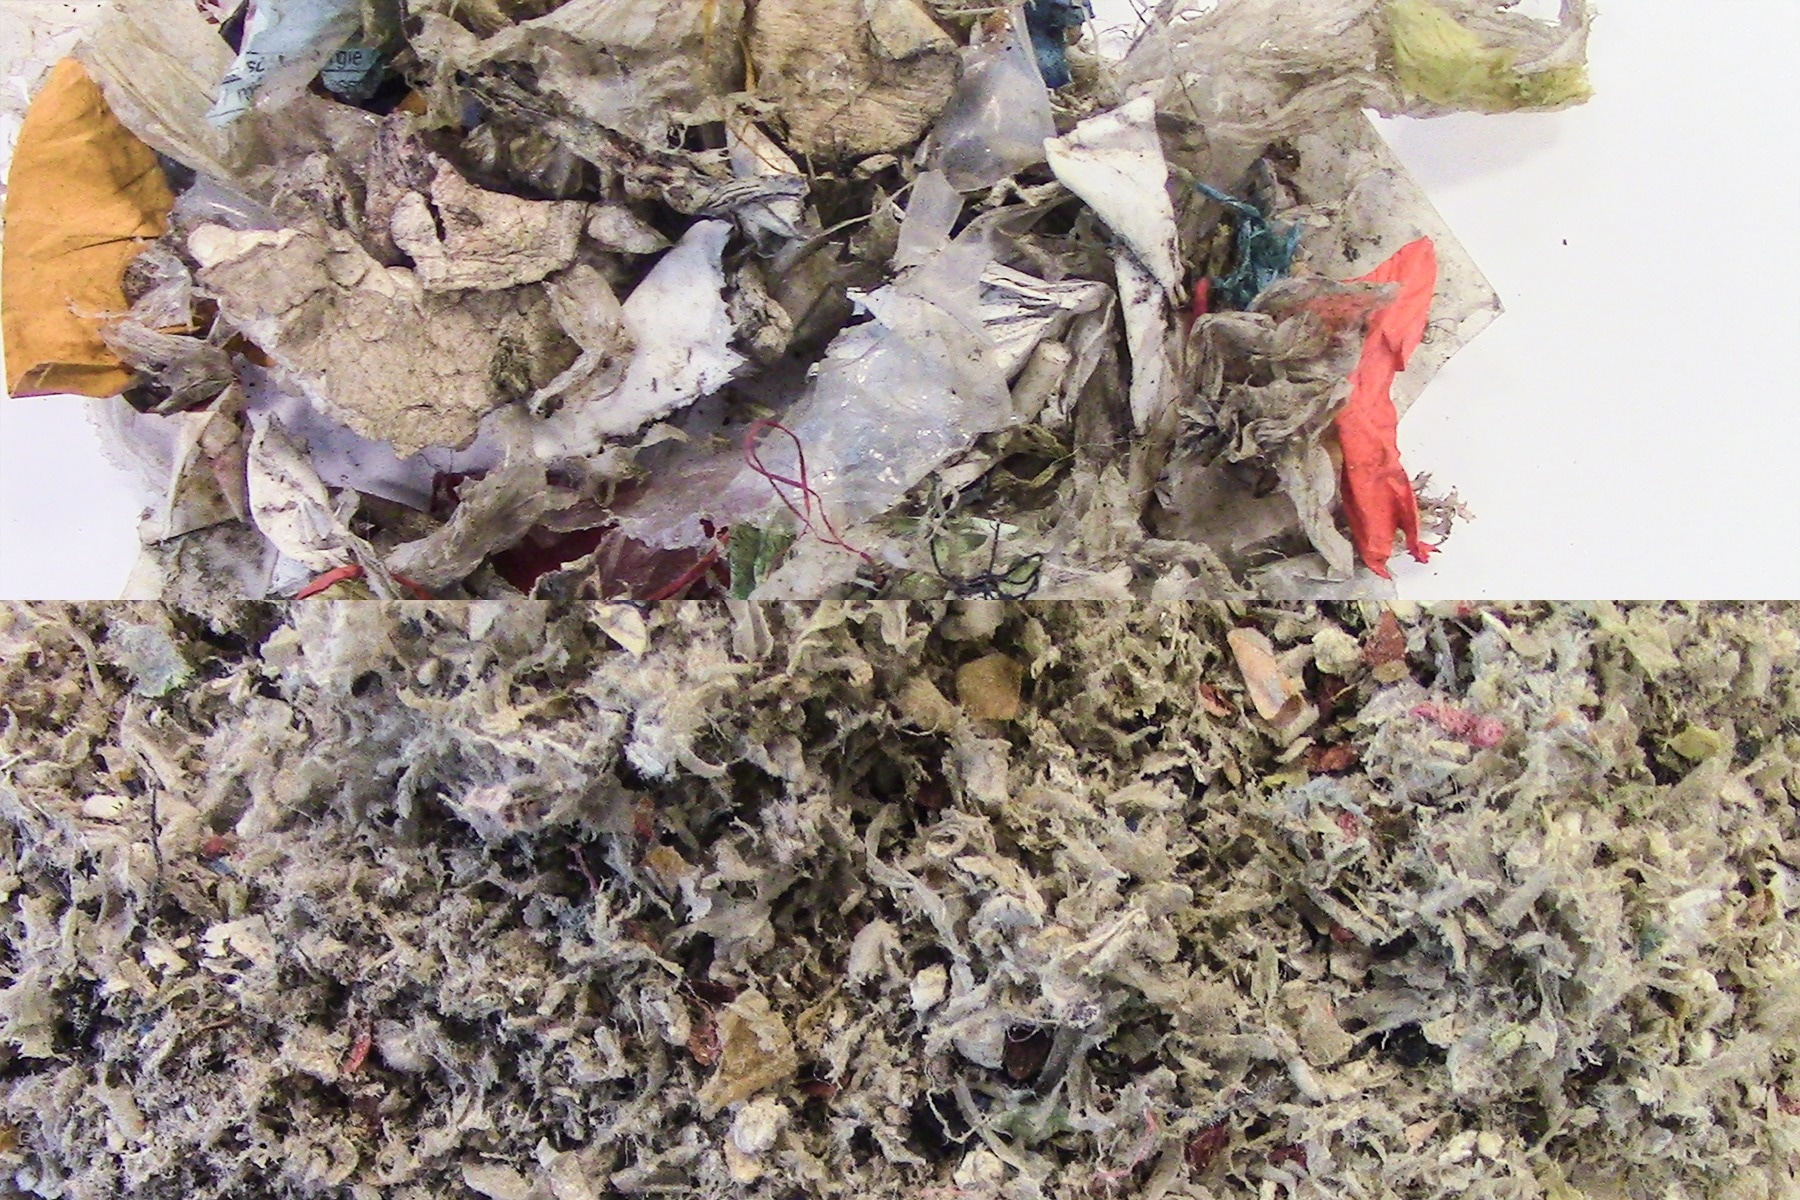
SM 300. 15 minutes | 6 mm. Image Credit: RETSCH GmbH
6 mm, 100 g
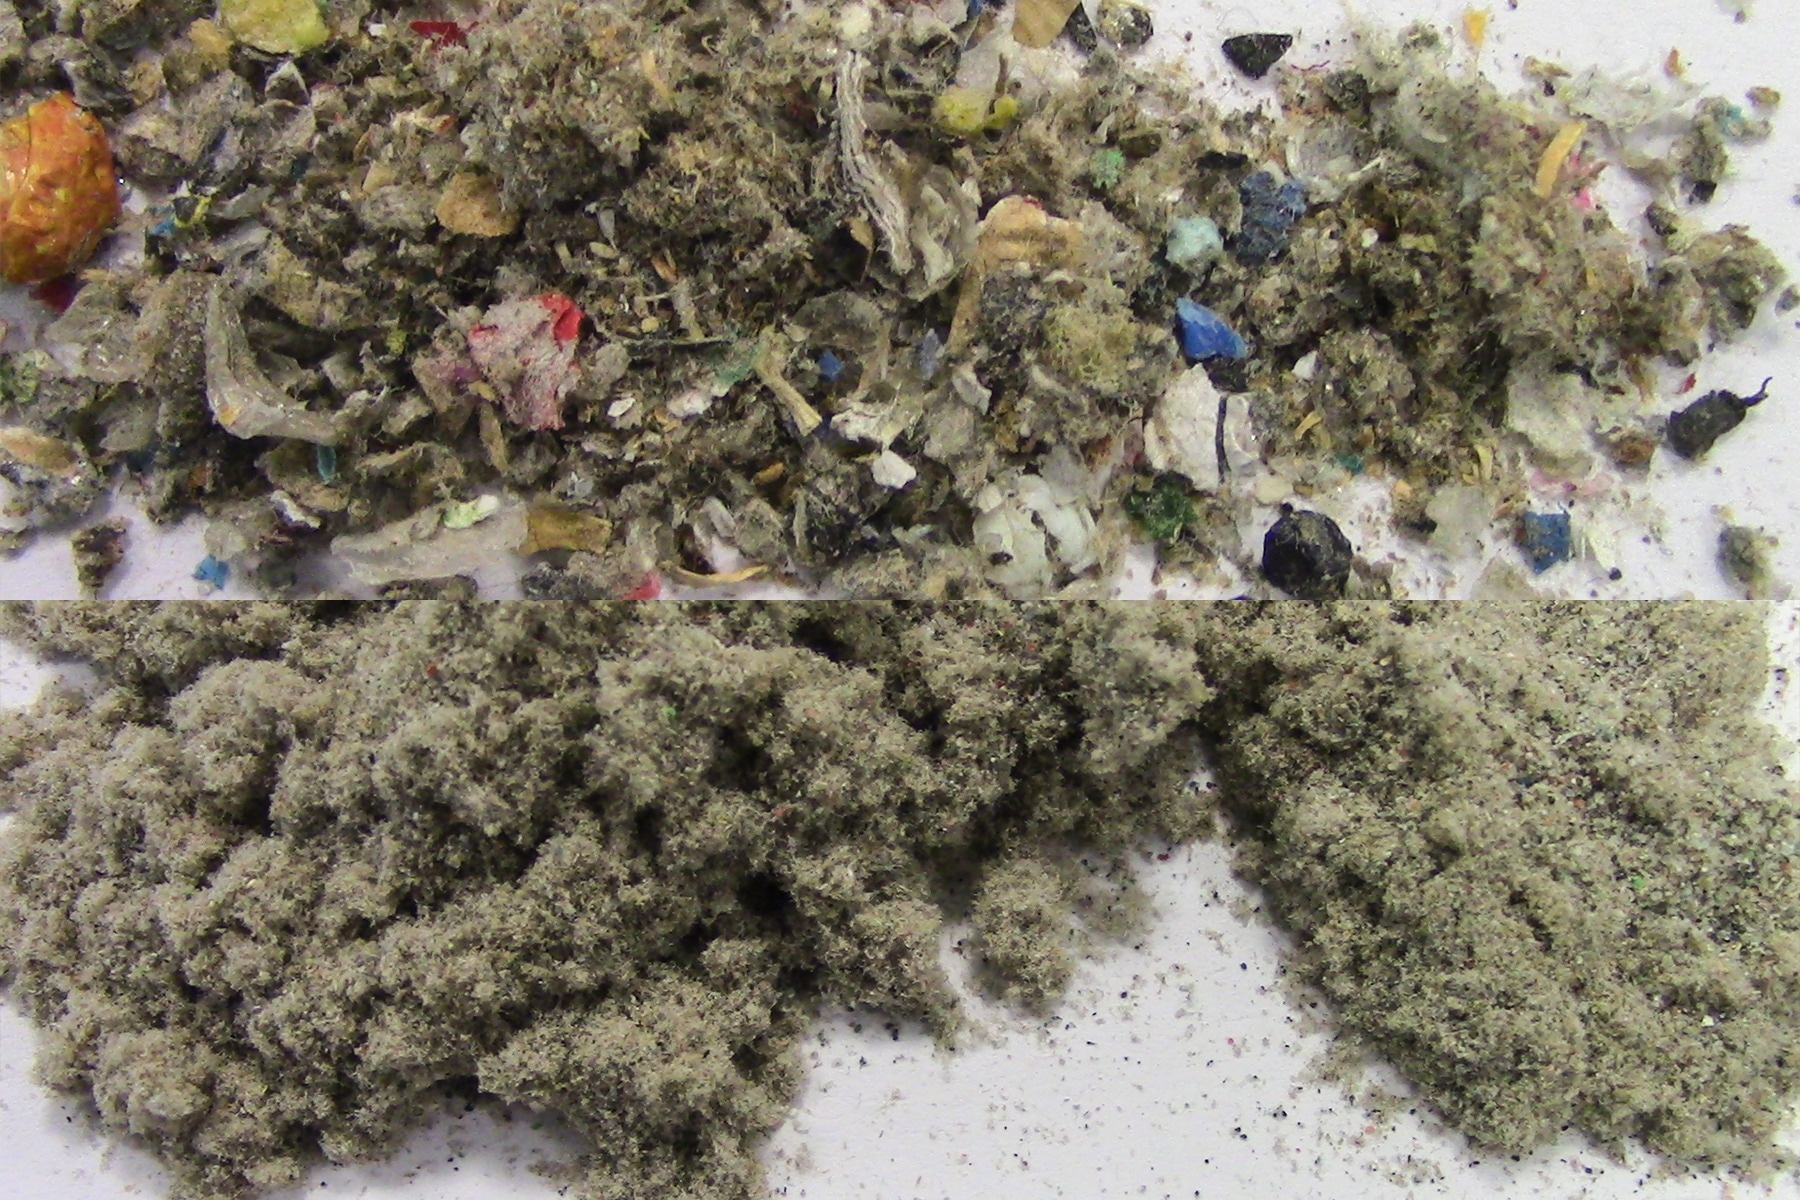
Pre-crushing SM 300. Fine-grinding ZM 300. 45 seconds | 0.75 mm. Image Credit: RETSCH GmbH
15 mm, 300 g
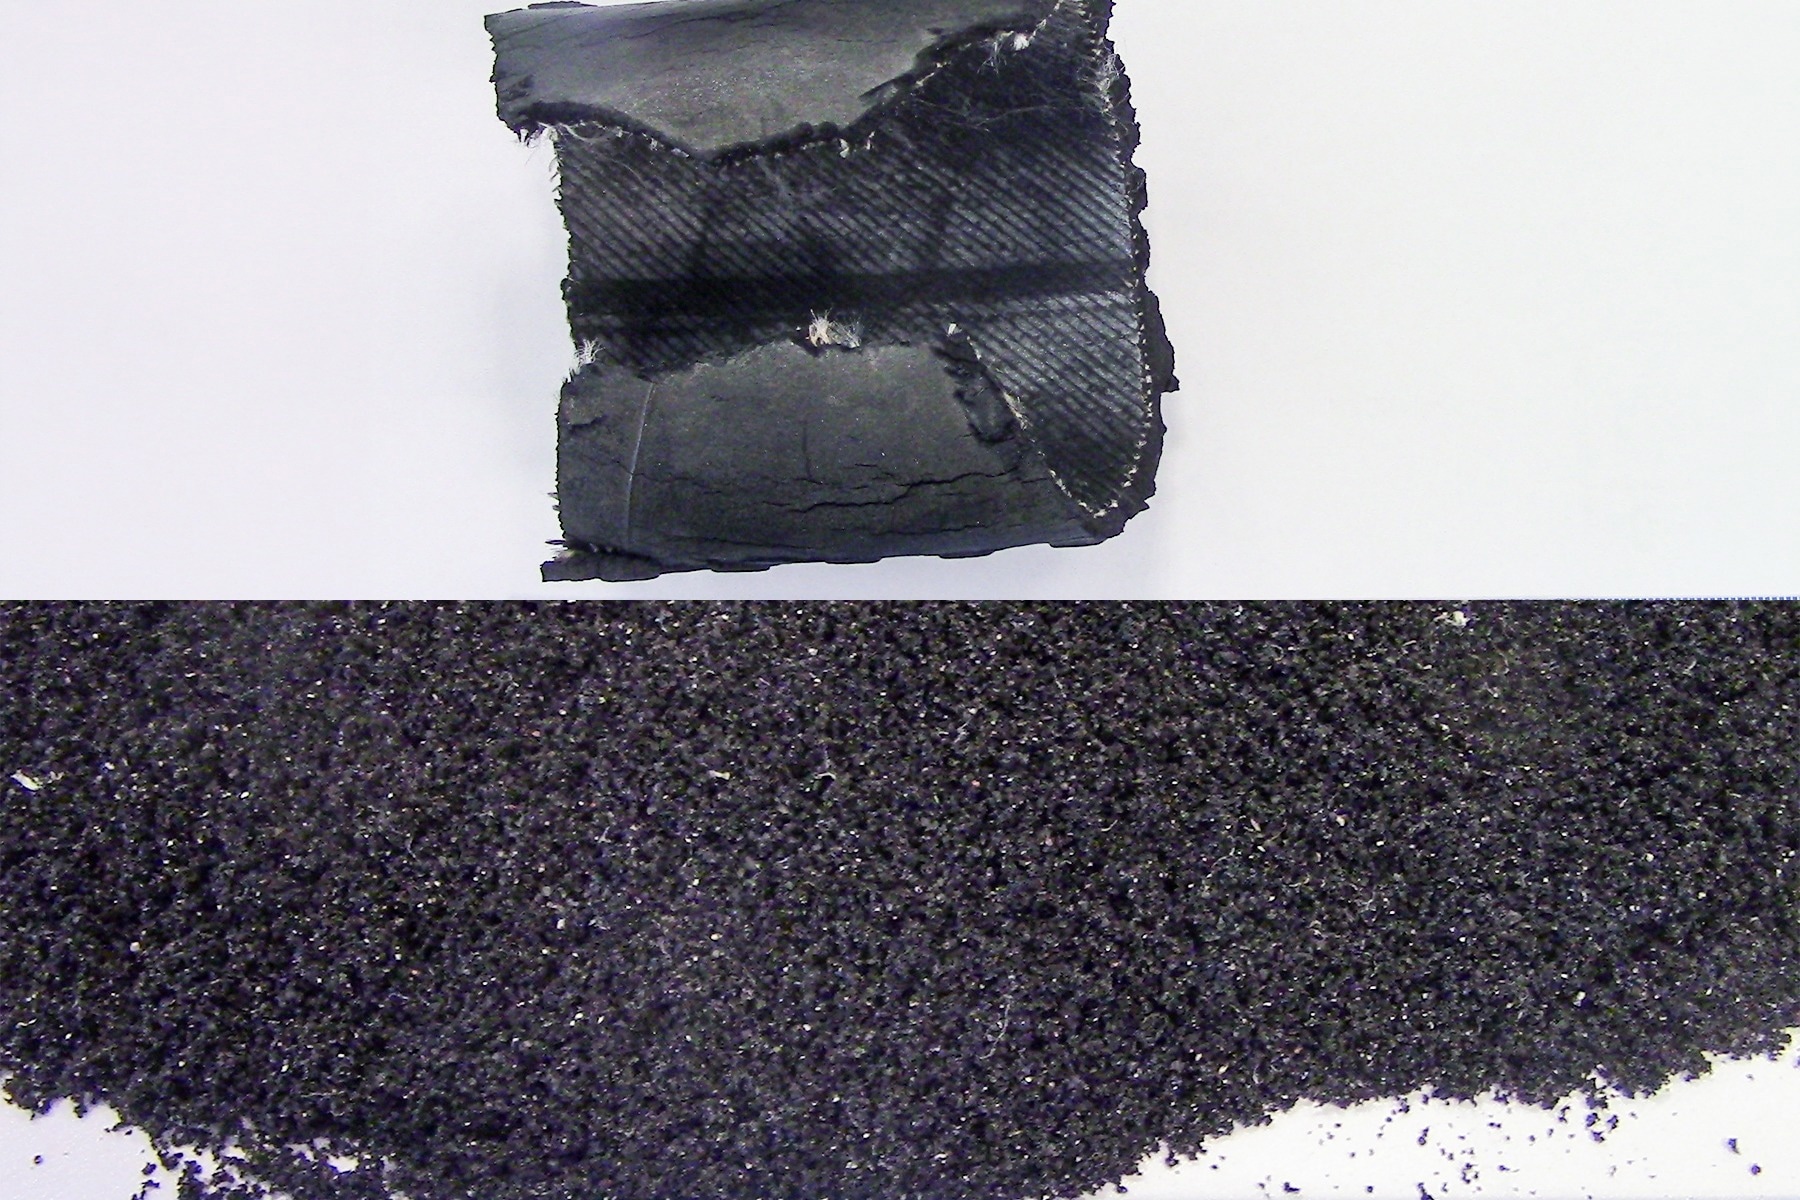
Pre-crushing SM 300. Fine-grinding ZM 300. 15 minutes | 0.3 µm. Image Credit: RETSCH GmbH
Biomass and Wood Residues
Biomass-based alternative fuels such as bark, wood chips, or demolition wood can be efficiently homogenized, provided the sample is pre-sorted and representative.
It is important to remove metal contaminants such as nails, screws, and staples before comminution to prevent analytical bias and protect cutting tools. Cutting mills are generally employed for coarse size reduction, followed by additional homogenization and milling with an appropriate sieve in the ZM 300.
Depending on the sample properties (for example, bigger twigs or more compact wooden blocks), it may be advisable to use the more robust six-disk rotor in the pre-cutting step rather than the standard parallel-section rotor.
Stable and reproducible processing can be ensured by employing a steady feed and optional cyclone operation in both the pre-crushing and fine-grinding steps.
Used Paper and Paper Rejects
Used paper and paper rejects typically demonstrate strong variability in terms of coatings, fillers, and moisture content, meaning that thorough homogenization is essential.
Cutting mills are ideally suited to the initial shredding step, and utilizing a V-rotor and pre-crumpling the material into smaller portions is key to improving cutting efficiency. The analytical portion can be milled in the ZM 300 after mixing and splitting to meet the requirements for elemental analysis, ash, or XRF.
Sewage Sludge as an RDF
Sewage sludge is typically wet and prone to agglomeration; it is important, therefore, to include a defined drying step (for example, using the TG 200) to ensure reproducible homogenization.
The material may be pre-comminuted in a cutting mill or jaw crusher after drying but before being thoroughly homogenized, to minimize local concentration effects of trace elements and ash-forming minerals.
The use of planetary ball mills such as the PM 400 is recommended for fine grinding and maximum homogeneity. Milling parameters must be able to achieve the desired fineness while limiting excessive heat buildup. This can be achieved by implementing a standardized drying and milling protocol, ensuring comparable analytical results over time.
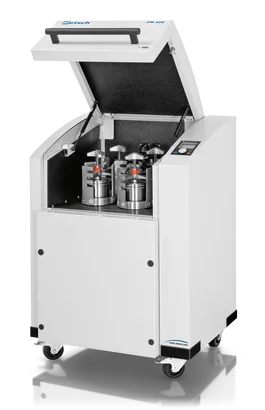
Image Credit: RETSCH GmbH
Wood Residues 125 mm, 800 g
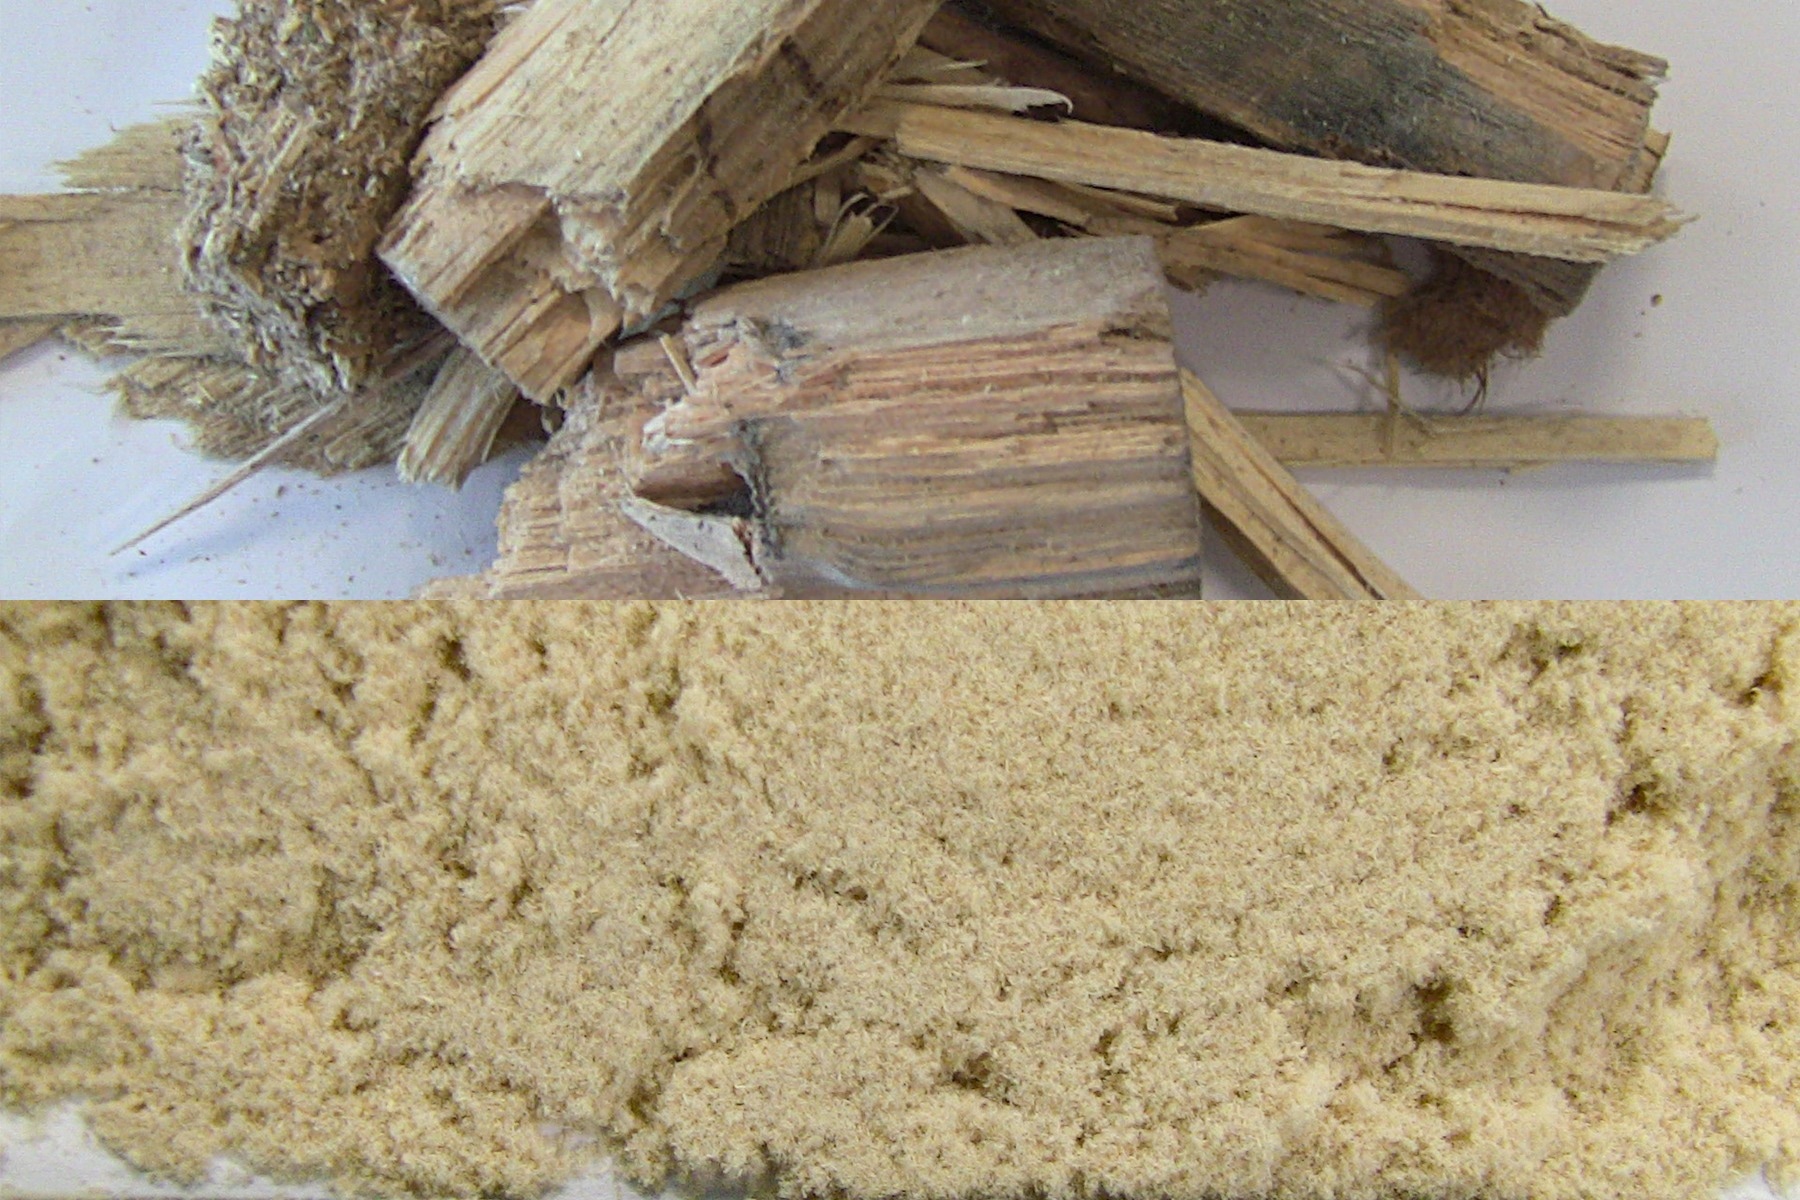
Pre-crushing SM 300. Fine-grinding ZM 300. Five minutes | 0.3 mm. Image Credit: RETSCH GmbH
Biomass 100 mm, 125 g
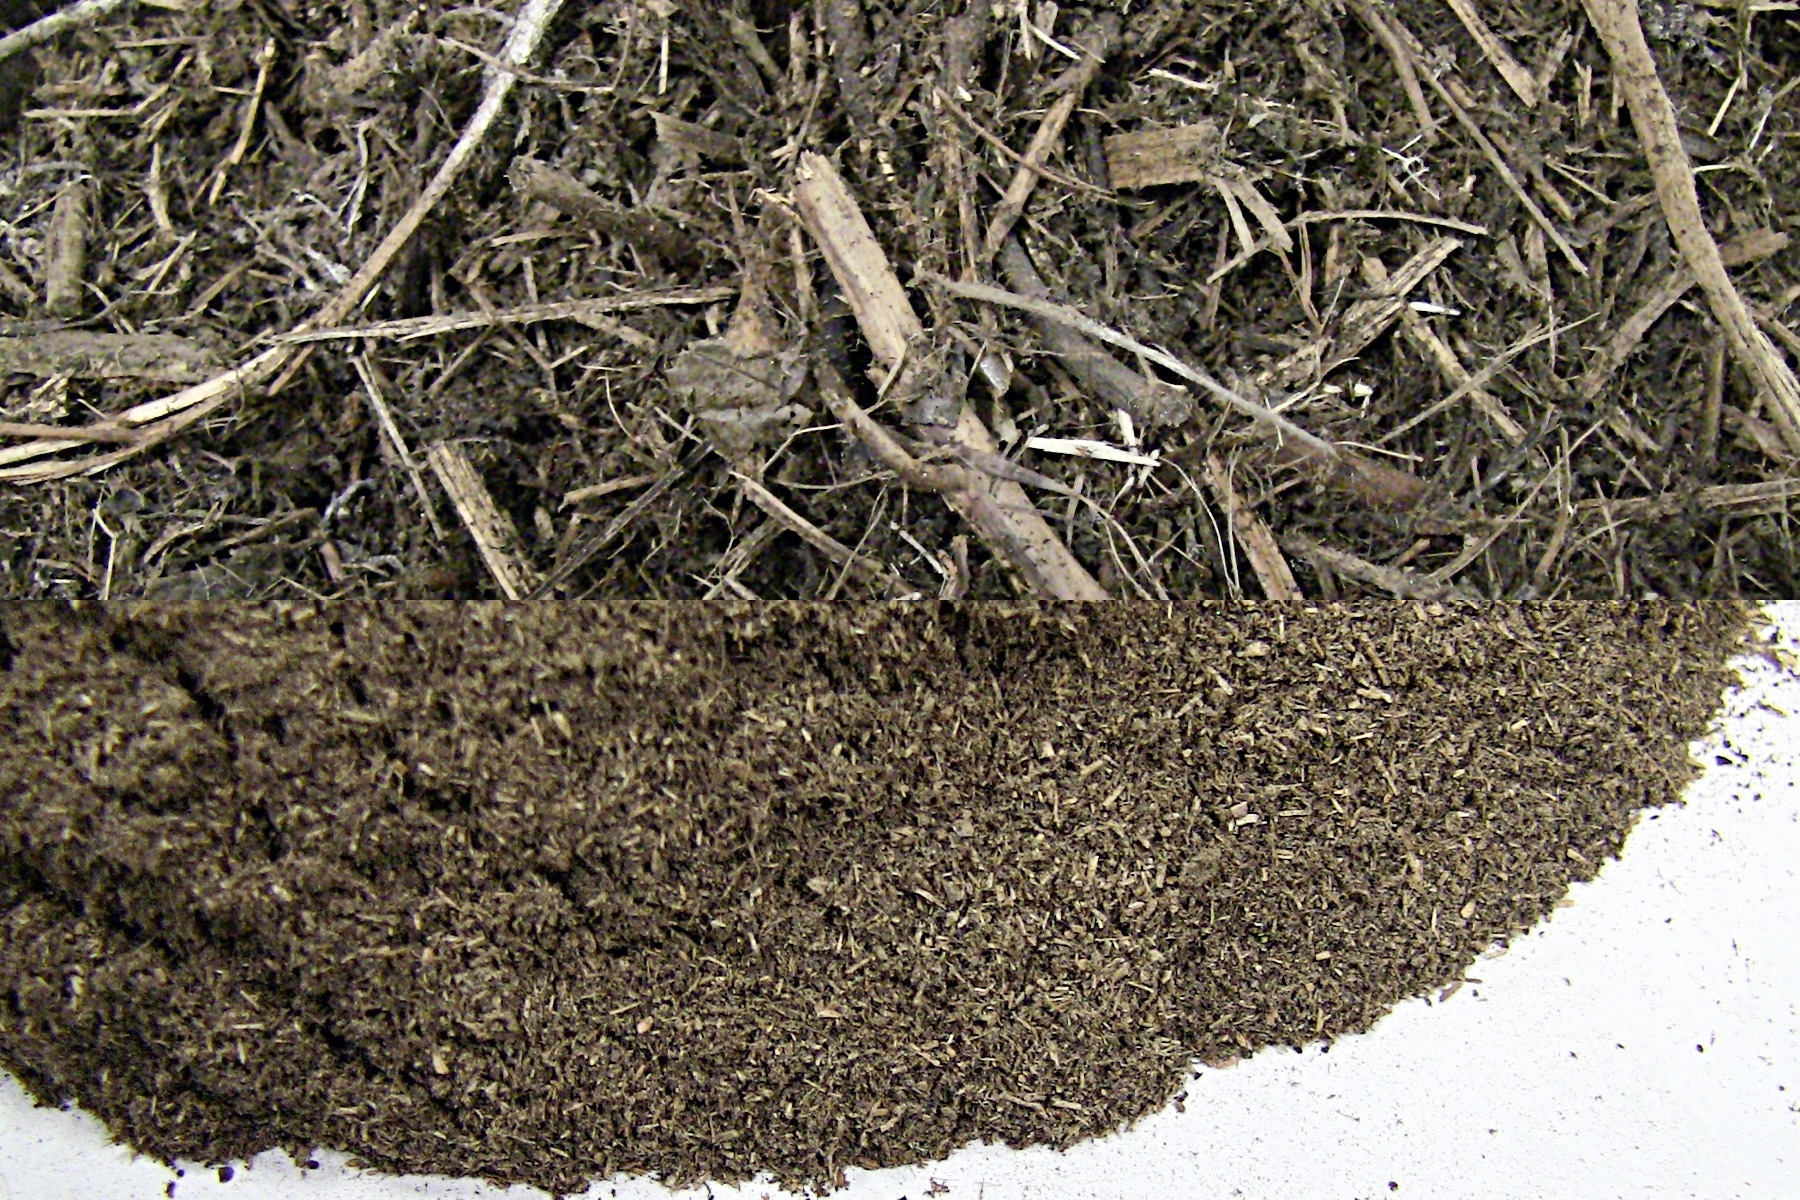
SM 300. Two minutes | 0.4 mm. Image Credit: RETSCH GmbH
Paper 50 mm, 7 g
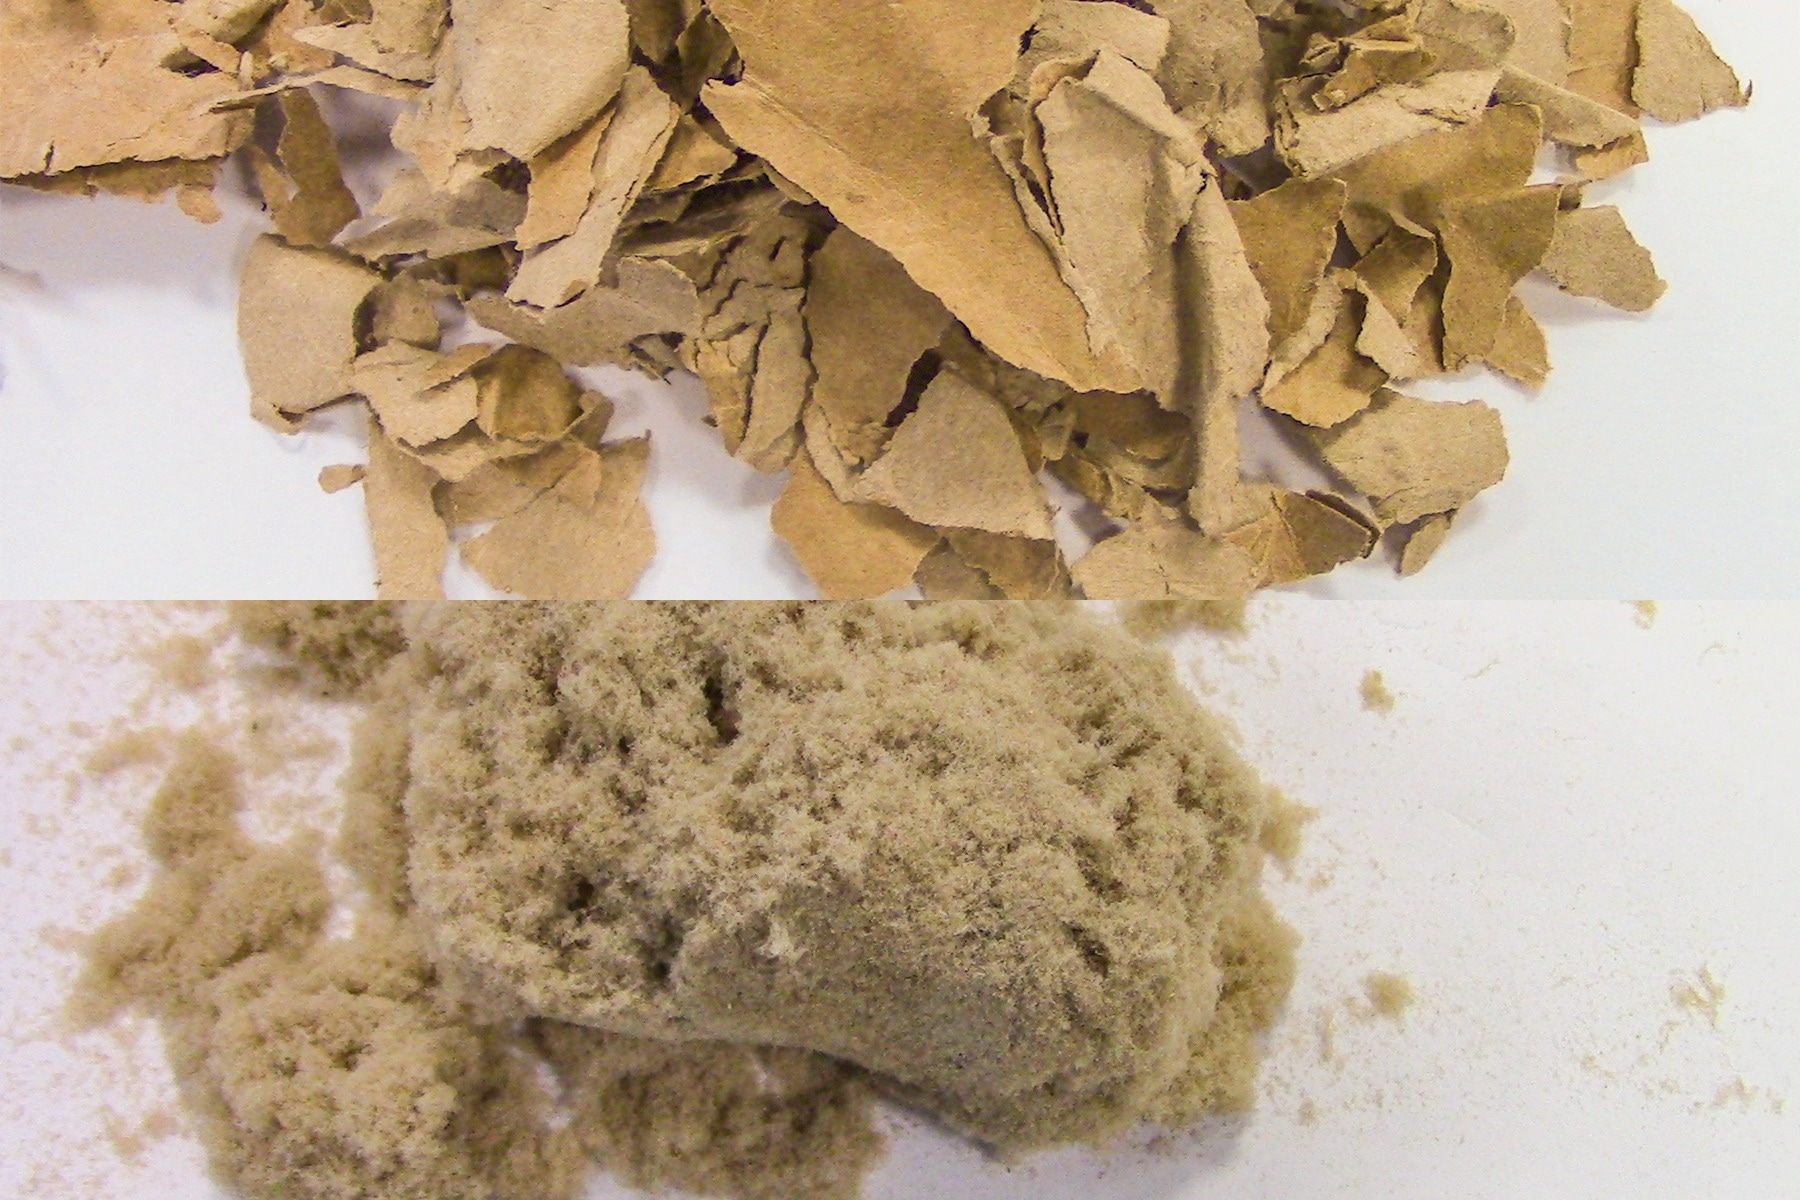
SM 300. 30 seconds | 0.6 mm. Image Credit: RETSCH GmbH
Dried Sewage Sludge 30 mm, 40 g
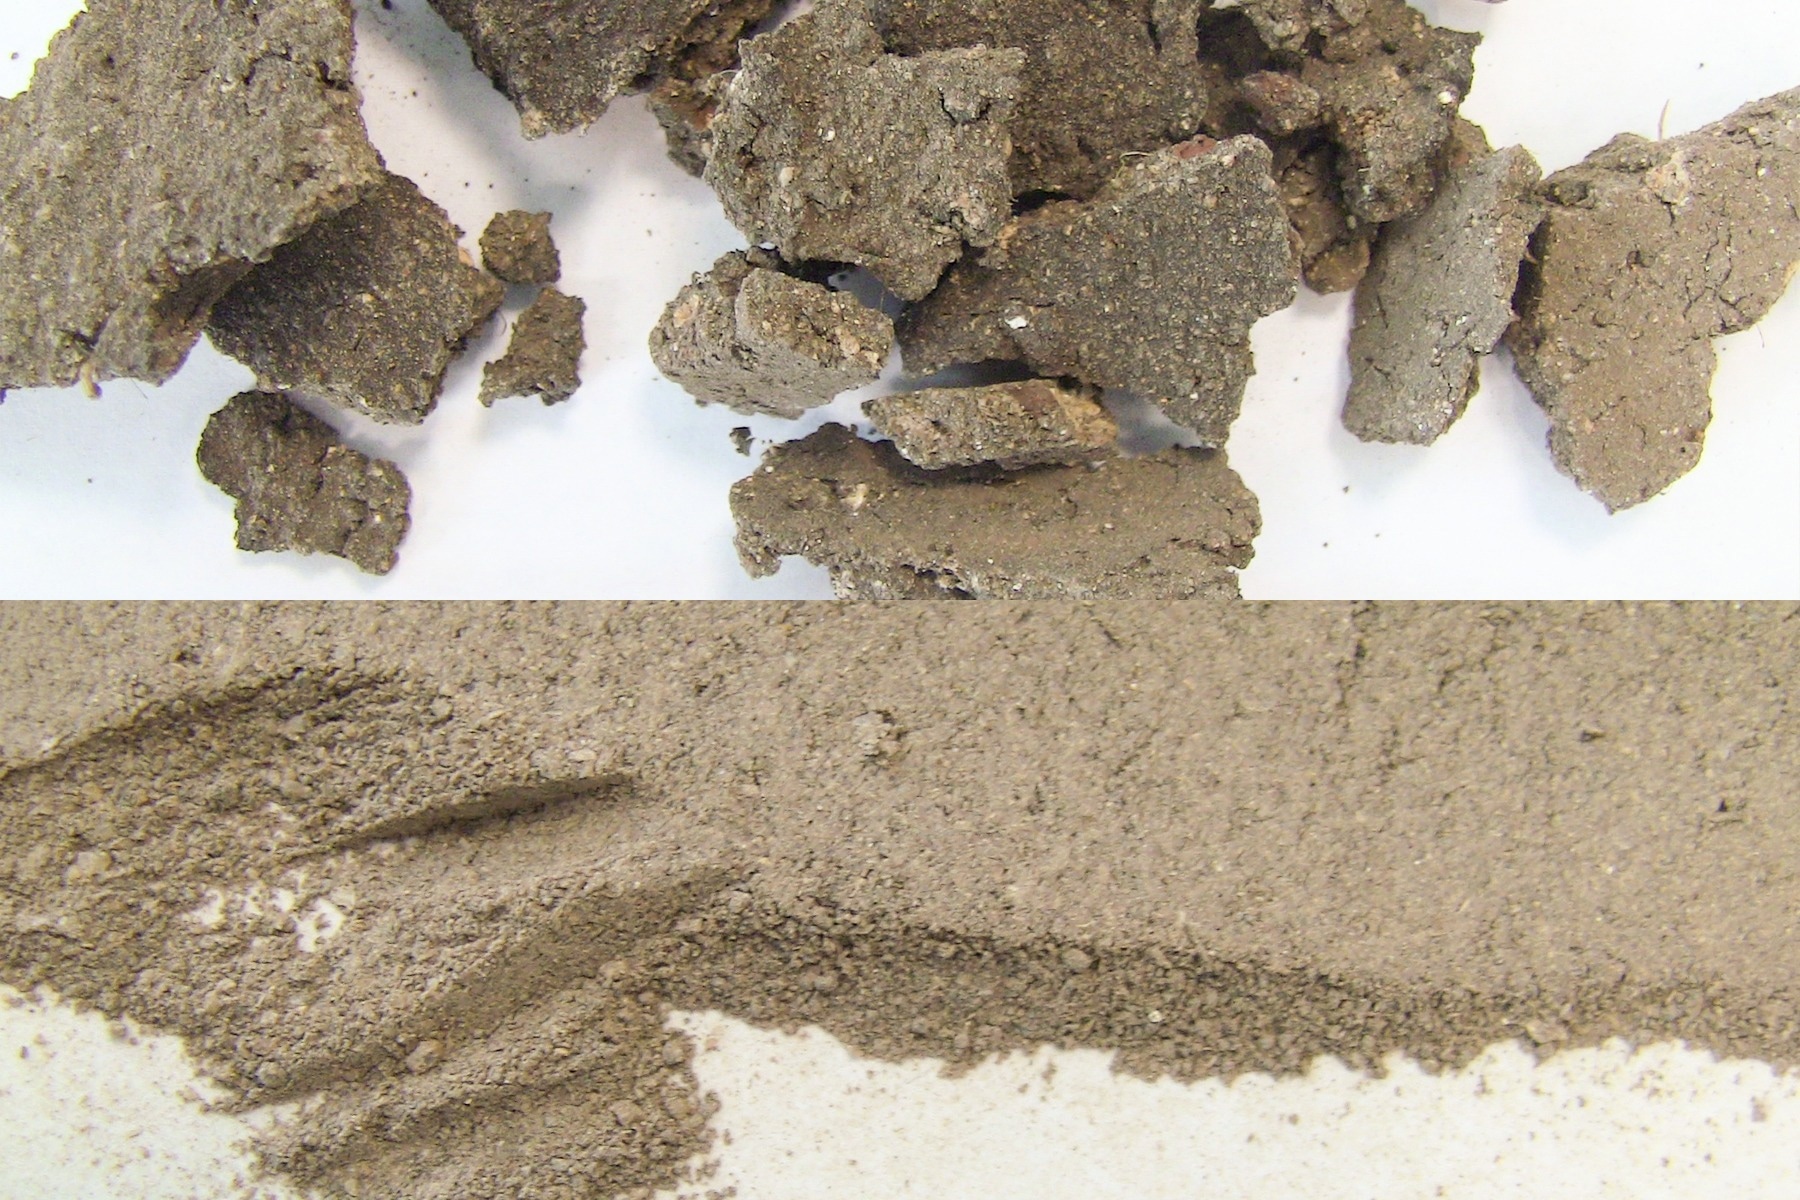
PM 400. 10 minutes | 0.2 mm. Image Credit: RETSCH GmbH
Asphalt Residues and Bitumen as Alternative Fuels
Asphalt residues can also be employed as alternative fuels in the cement industry, because the bitumen content has a usable calorific value.
One way asphalt materials can be used is to feed them into a cement kiln for energy recovery after appropriate processing, partially replacing fossil fuels. Careful sorting, impurity removal, and strict quality control are essential if the material is to be used as an alternative fuel.
Ensuring defined bitumen content and the analysis of potential contaminant loads is also especially important.
Asphalt residues can contribute to resource conservation when used as alternative fuels in the cement industry, as well as enabling the more efficient use of mineral waste streams.
Bitumen makes asphalt sticky, however, meaning that embrittlement with liquid nitrogen is required during the fine crushing stage. The SK 300 crossbeater mill is well-suited to this purpose, because it is robust and resistant to abrasive materials.
Asphalt with a Bitumen Content
110 mm, 11.7 kg
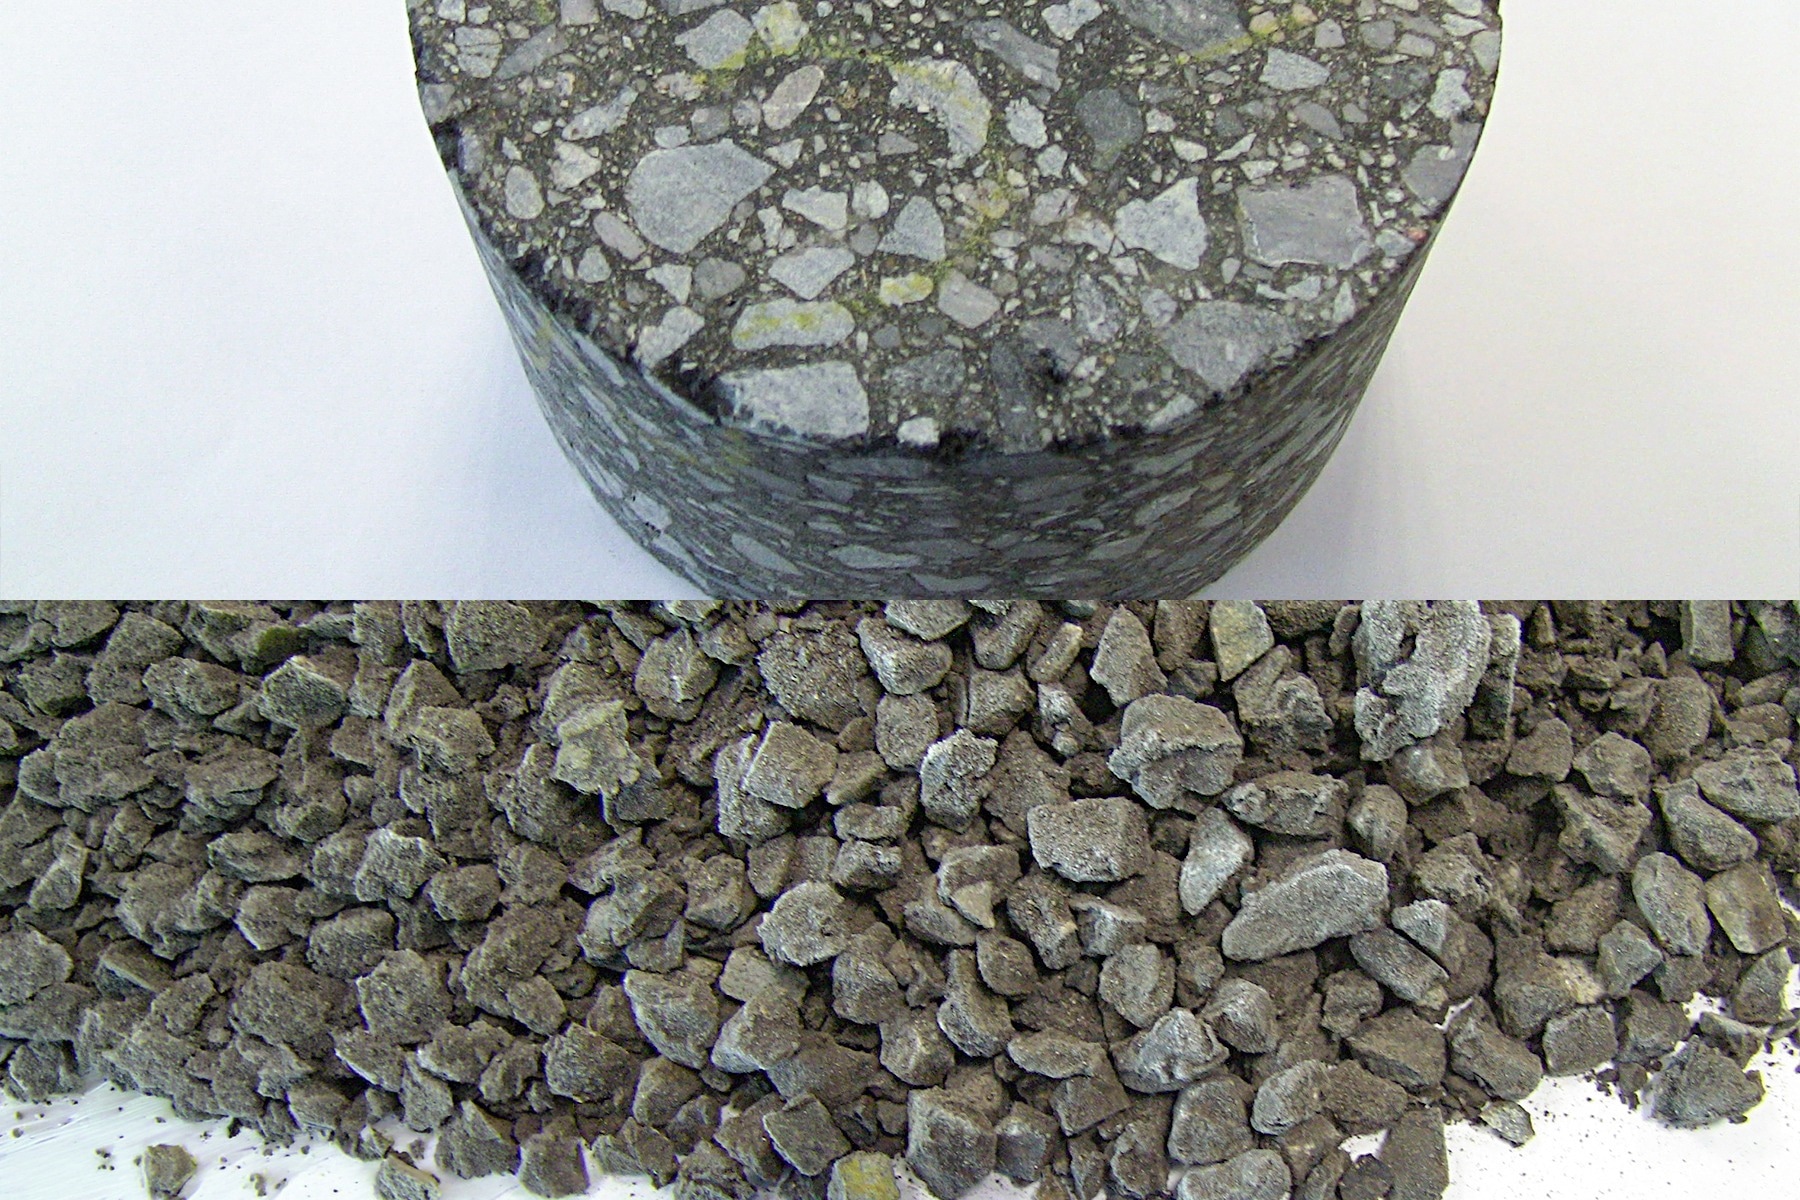
BB 300. One minute | 8 mm. Image Credit: RETSCH GmbH
10 mm, 1.7 kg
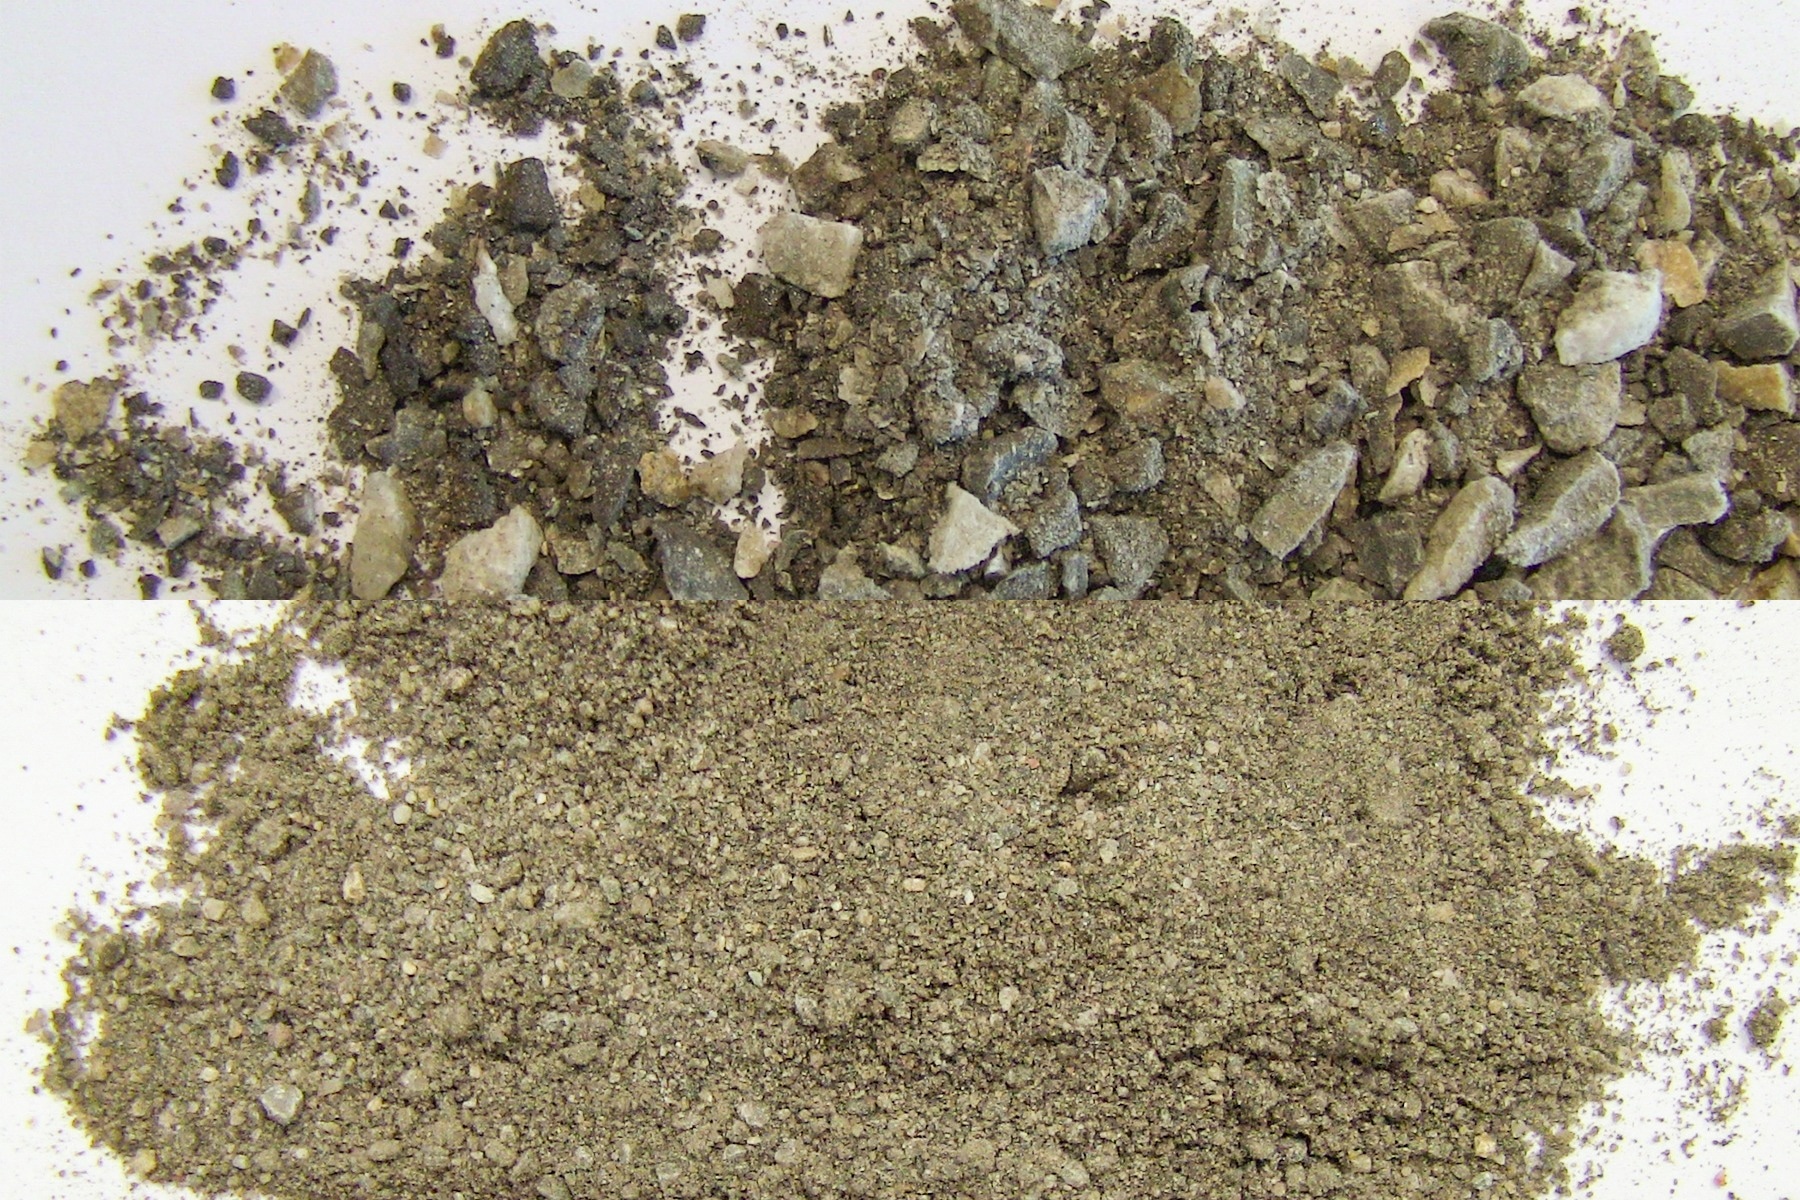
SK 300. 90 seconds | 1 mm. Image Credit: RETSCH GmbH
Old Textiles and Textile Waste as Alternative Fuels
Old textiles and textile waste can be used as alternative fuels in the cement industry, with textiles playing a key role as secondary fuels in cases where material recycling is no longer viable.
A large number of textile residues have a usable calorific value due to their organic content. These residues can, therefore, partially replace fossil fuels in cement kilns after appropriate processing.
Materials destined for use as a secondary fuel are sorted, shredded, and homogenized before being tested for impurities and contaminants. Their use is especially relevant in processed fuel mixtures, where it is possible to use textiles along with other high-calorific waste materials.
Using textile waste as a secondary fuel can help contribute to a more resource-efficient and circular cement industry.
Textile homogenization for quality control typically begins in a cutting mill, followed by fine grinding in the ZM 300 or a ball mill.
Textiles
200 mm, 20 g
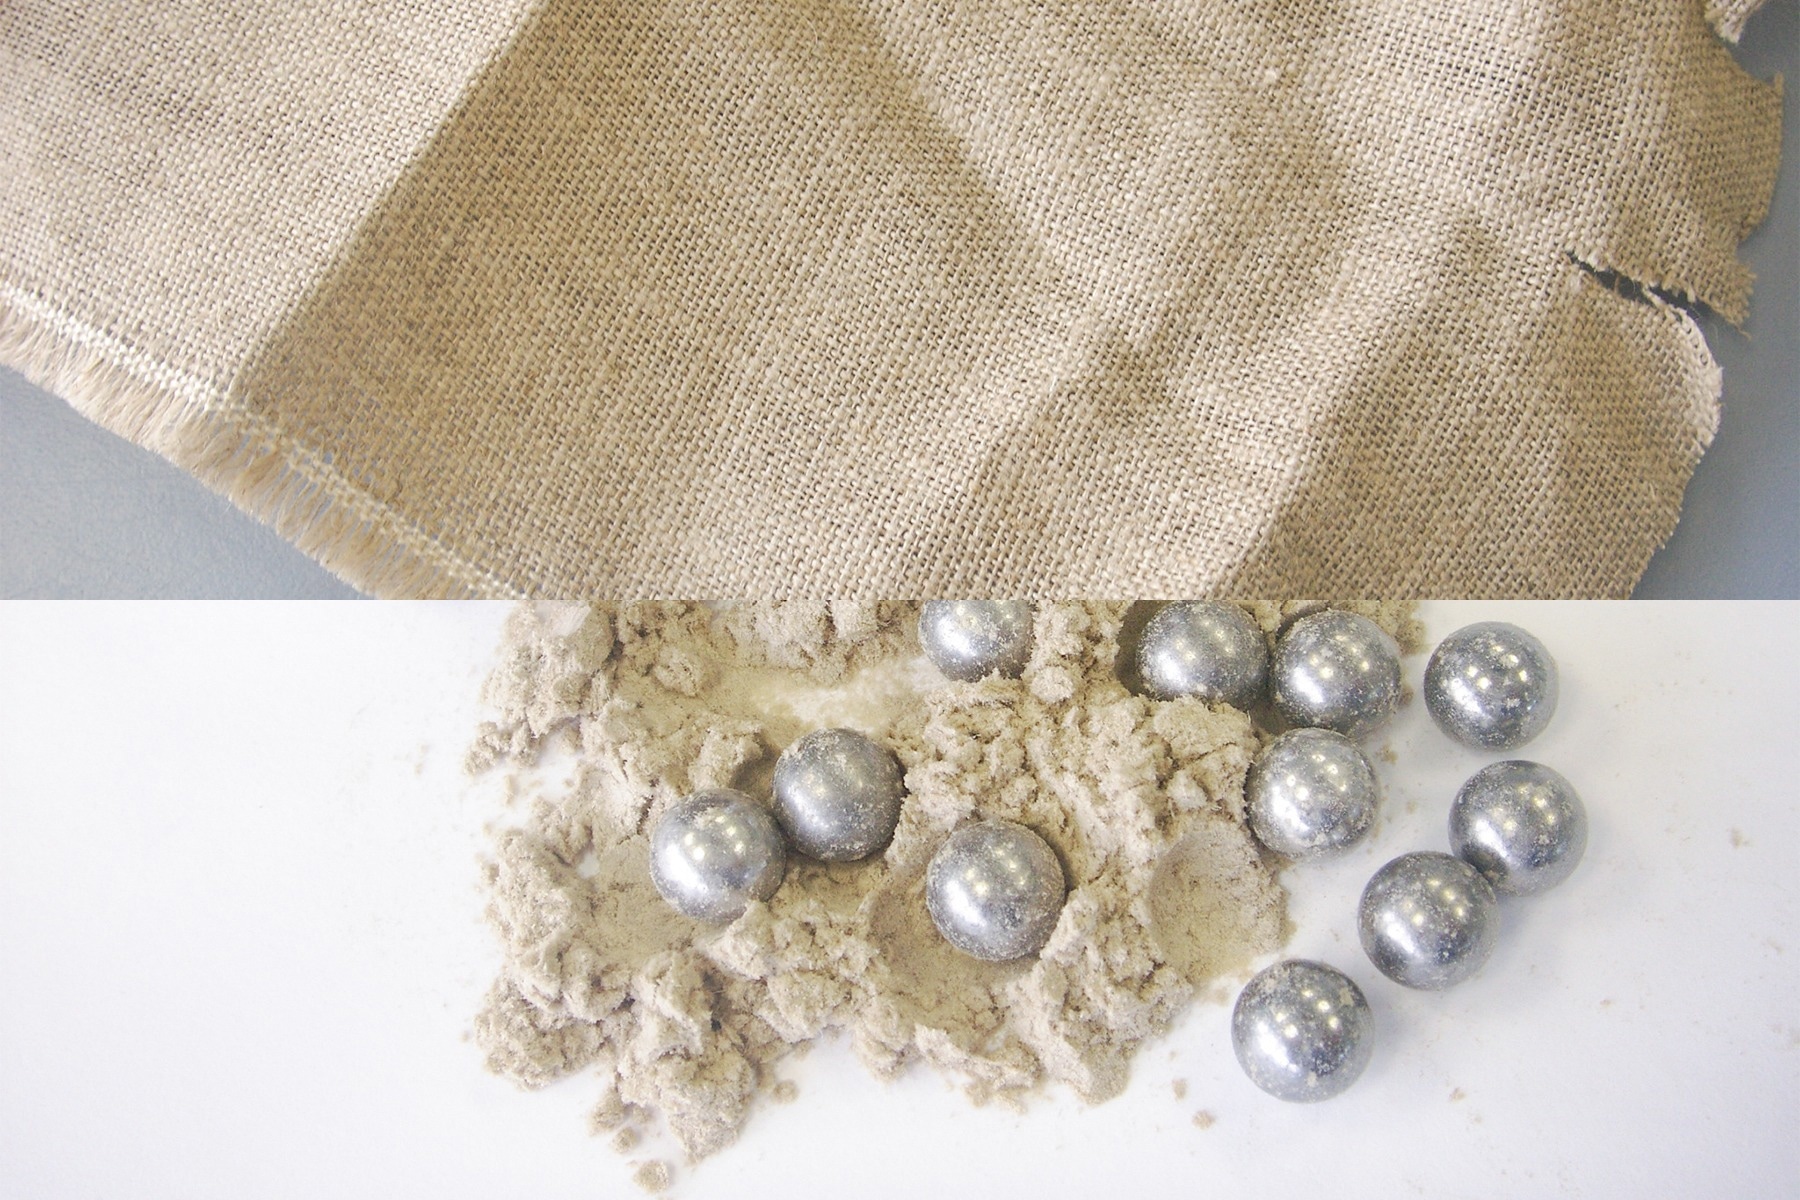
Pre-crushing SM 300. Fine-grinding MM 400. 2 min | 200 µm. Image Credit: RETSCH GmbH
RDFs as a Reliable Alternative to Fossil Fuels
RDFs and other alternative fuels offer a reliable, sustainable means of reducing fossil fuel consumption in cement manufacturing.
These fuels must be properly sampled, prepared, and analyzed, however, with robust homogenization strategies, standardized laboratory workflows, and material-specific preparation techniques underpinning regulatory compliance, consistent kiln performance, and long-term process optimization.
This information has been sourced, reviewed, and adapted from materials provided by RETSCH GmbH.
For more information on this source, please visit RETSCH GmbH.